
Industries Served
AGS Middle East FZE provides engineered solutions across seven core industrial sectors. Combining Swiss-manufactured ChemValve fluoropolymer-lined valves with certified electrical distribution and automation systems, we safeguard plant integrity in the most demanding operating environments.
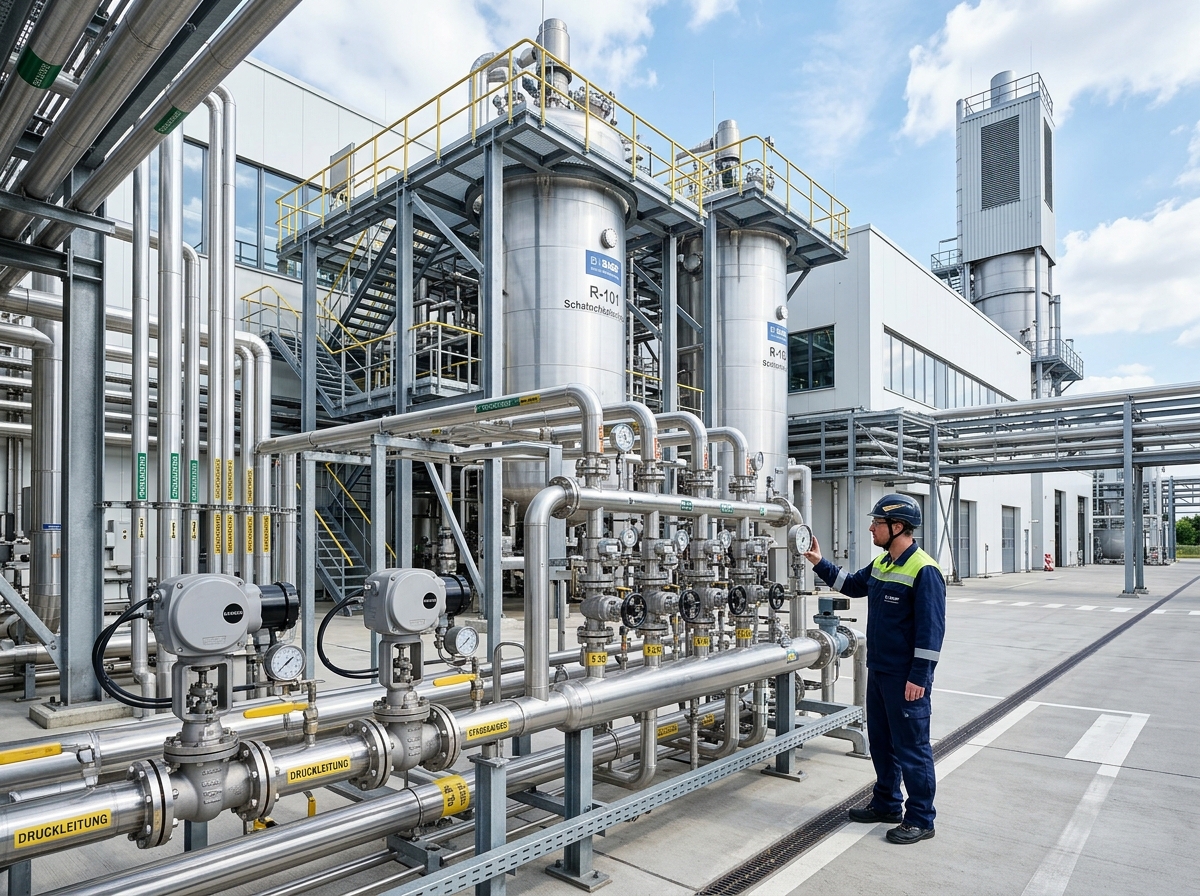
Chemical
Safe handling of aggressive chemicals, chlor-alkali streams, concentrated acids, and volatile reagents with zero-leakage ChemValve PTFE-lined valves and ATEX certified electrical junction boxes.
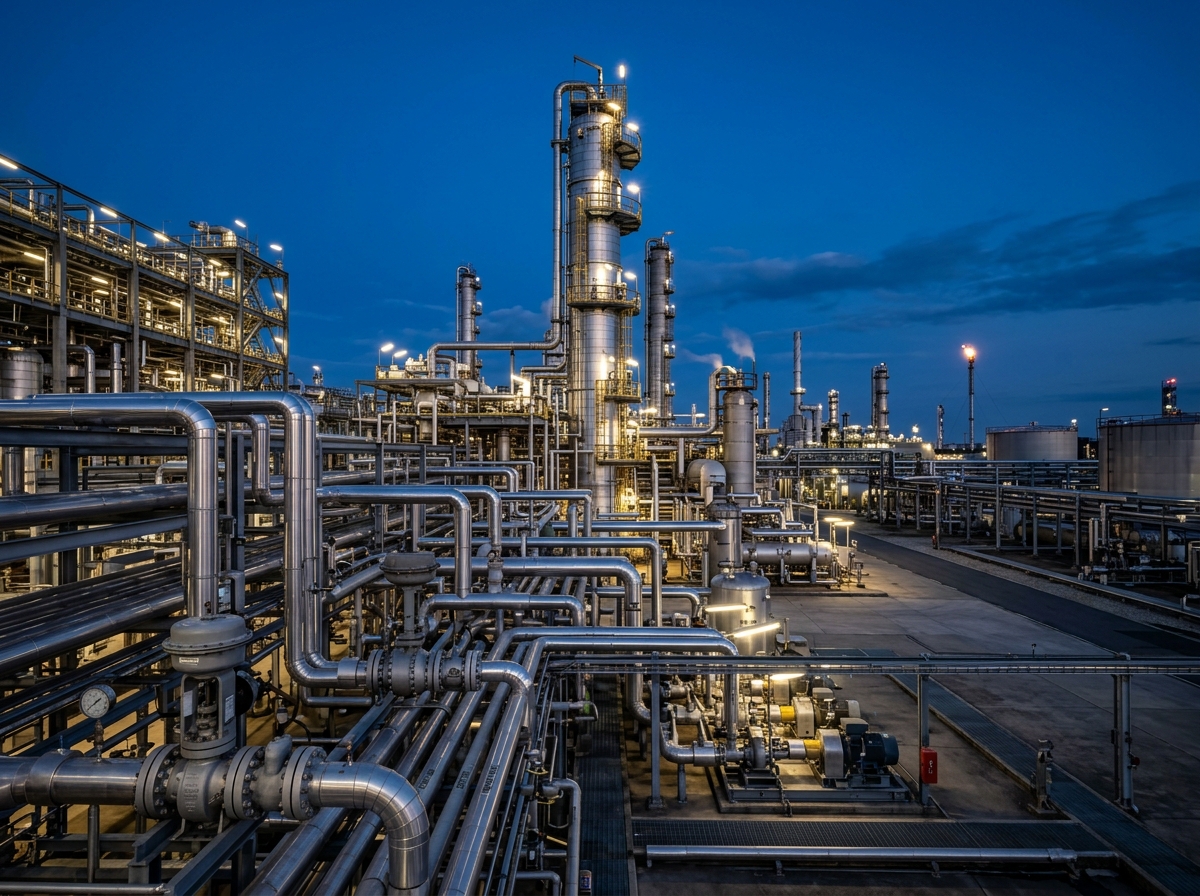
Petrochemical
High-temperature and high-pressure fluid isolation for refineries, gas fractionators, and hydrocarbon processing units requiring strict emissions compliance and certified power distribution.

Mining
Heavy-duty abrasive slurry transport, acid heap leaching, and mineral refining systems with wear-resistant lined check valves, heavy cable protection, and robust switchgear.

Food
FDA-compliant non-contaminating valve solutions and washdown-safe electrical enclosures for beverage processing, dairy lines, starch refining, and food-grade packaging automation.

Environmental Technology
Industrial wastewater treatment, flue gas desulfurization (FGD), acid recovery loops, and scrubber systems equipped with corrosion-proof lined check and butterfly valves.

Pulp & Paper
Bleaching plant pipelines, chemical recovery boilers, chlorine dioxide handling, and fibrous pulp slurries managed via non-stick PTFE linings and moisture-sealed cabling.
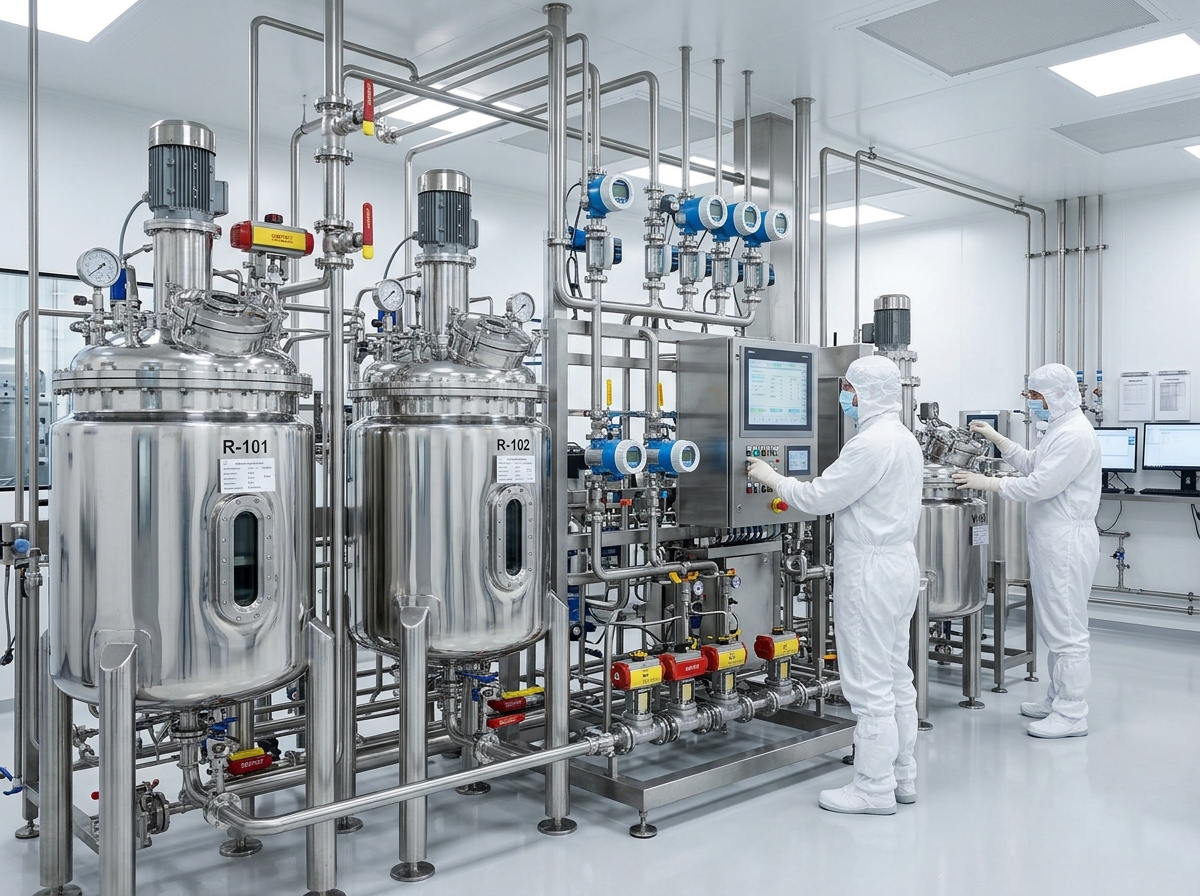
Pharmaceutical
High-purity active pharmaceutical ingredient (API) synthesis, aggressive solvent recovery, cleanroom power distribution, and sterile media isolation with zero batch contamination.
Looking for Application-Specific Engineering?
Our technical sales team in Ajman Free Zone assists process engineers with valve material selection, actuator sizing, and power distribution architectures tailored to your facility parameters.